Packing PPGI Coils Without Damaging the Coating
PPGI packaging fails at the edges and the coating, not at the wrapper. This guide covers protector rules, contact materials, changeover contamination, and the acceptance checks that keep coated coils defect-free.
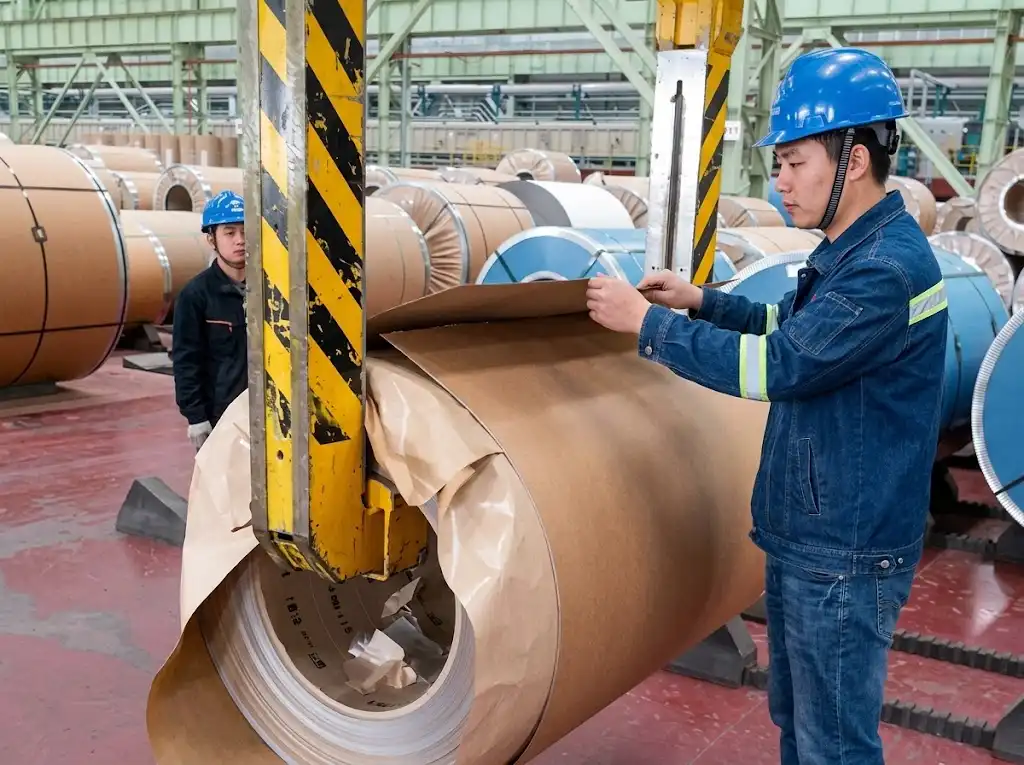
PPGI Coil Packing Line: Preventing Edge and Surface Damage
PPGI Coil Packing Line: Preventing Edge and Surface Damage
PPGI coils bring two packaging challenges together at the same time: the coating must be protected as a visible finished surface, and the coil edges often need careful support so the package survives handling without creating rub marks, pressure points, or chipped areas. A general steel-coil package can look complete and still be wrong for PPGI if it ignores coating sensitivity, edge protection, or contamination from a previous product run.
This article is for packaging, production, and quality teams that need to define an automatic coil packing line for pre-painted or similarly coated coils with clear attention to edge and surface damage prevention.
Start with Coating Sensitivity and Package Route
PPGI packaging should begin with the real coating and shipment condition the team needs to protect. The line must consider whether the coil will be stored briefly indoors, staged for longer periods, shipped domestically, or prepared for export. Those route conditions affect the package build, but the first decision is still local: where can the coating be damaged while the coil moves through the line?
The common risk points are not only during wrapping. They include infeed support, side guidance, protector placement, strapping contact, stack compression, and any transfer where the coil can shift.
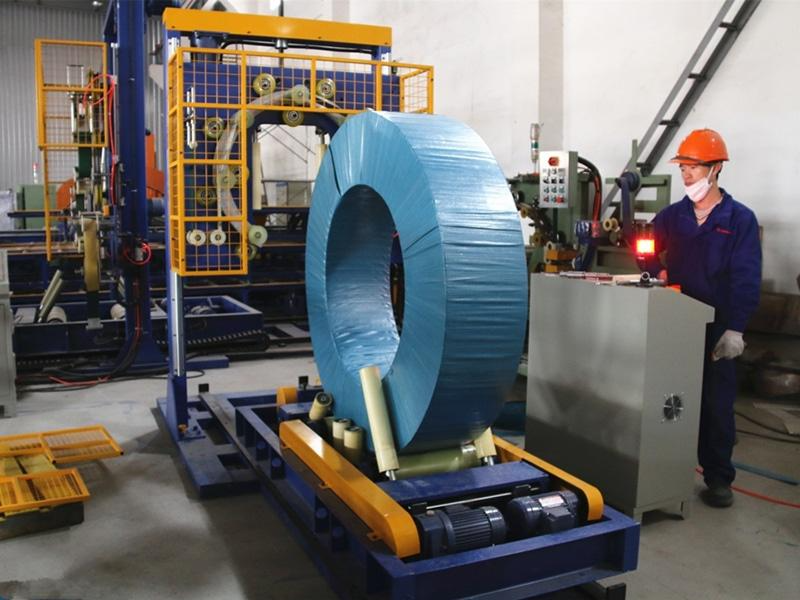
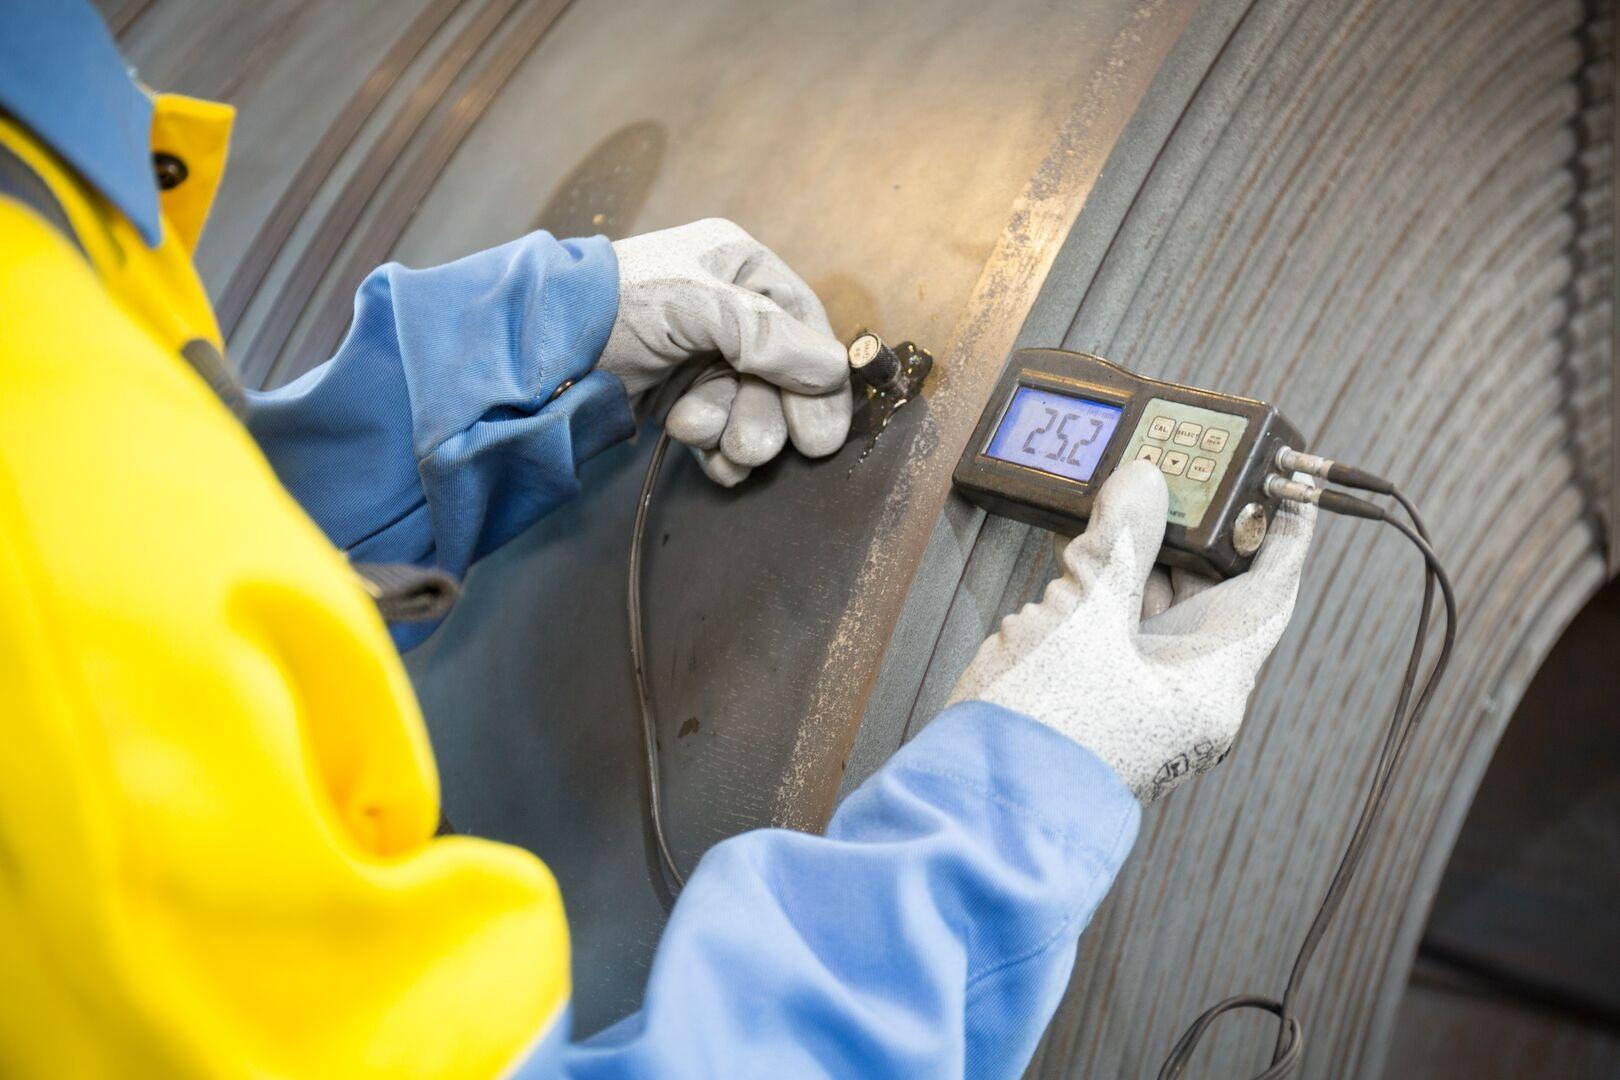
The image shows an automatic steel coil packing machine with an operator nearby. The finish risks begin before the wrapper: infeed support, side guidance, protector placement, and transfer can all touch the coating while the coil moves through the line.
Edge Protection Is Structural, Not Decorative
For PPGI, edge protection should be treated as part of the package structure. If the edge protector is underspecified, misplaced, or incompatible with the line's handling path, the package may cut into the coating or allow damage when the coil is lifted, stacked, or strapped.
The specification should define:
- Which products require edge protection
- Protector type and contact arrangement
- When corner or side-face protection is added
- How protector placement is checked before the coil continues
- What happens when a protector slips or is missing
Without that detail, "edge protected" is only a label.
Surface Protection Needs the Right Layer Sequence
Coated products are sensitive to contact marking, trapped debris, and pressure from the wrong material arrangement. The package recipe should define which layer touches the painted surface, which layer separates or cushions, and which outer layer provides package integrity for handling and storage.
The order matters. A line that uses the correct materials in the wrong sequence can still create a surface problem. That is why PPGI packaging should be documented as a build sequence rather than a generic material list.
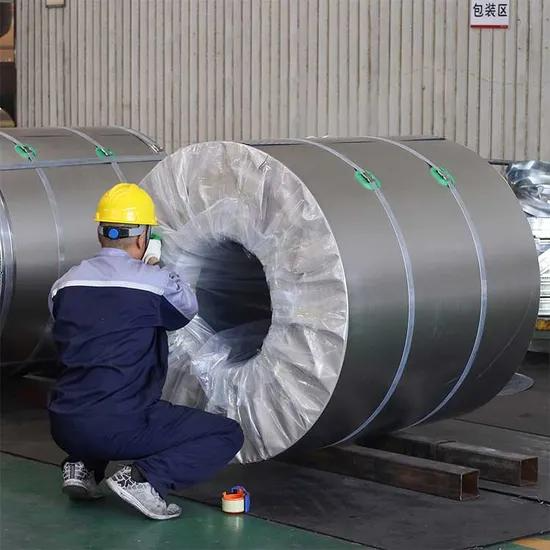
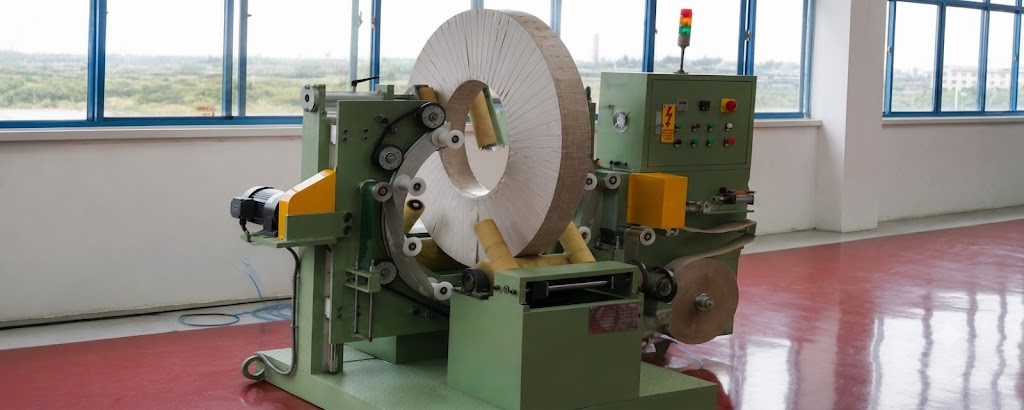
The image shows an automatic film application station with an operator nearby. The recipe defines which film layer touches the coated surface and how the sequence is applied without trapping debris under the package.
Watch coil packing machinery and a coil stretch wrapper in operation:

Control Sleeves, Pads, and Strap Contact
Where strapping is part of the package, the project should define how sleeves, pads, protectors, or other approved contact devices keep the strap load from concentrating on the coating or edge. It is not enough to say the strap is used carefully. The line should specify the approved contact arrangement and inspection point.
This is particularly important when the same line handles other steel products that may not require the same contact precautions.
Changeover Contamination Is a Real Packaging Risk
Mixed-product lines often fail on changeover discipline. Residual debris, damaged protectors, unsuitable pads, or the wrong material reel from the previous job can turn a correct PPGI recipe into a defective package run.
That means the line should define a changeover reset for coated products:
- Clear previous scraps and loose particles
- Confirm approved contact materials are loaded
- Check protectors, sleeves, and pads
- Run a first article and review the visible result
If the line handles bare steel, stainless, and coated products together, this reset becomes even more important.
Separate Coating Protection from Corrosion Claims
PPGI packaging discussions often mix two different concerns: preserving the painted surface and managing corrosion-related exposure. Those are connected, but they are not the same decision. A package can protect the coating from contact damage and still need separate review for storage or export moisture conditions.
Keeping those boundaries separate helps the team avoid unsupported claims and write a more useful specification.
Acceptance Must Focus on Edge and Surface Outcomes
The acceptance plan for PPGI should not stop at package appearance. It should verify whether the edge and coated faces remain within the site's approved visible condition after the real packaging and handling sequence.
Useful checks include:
- Correct layer sequence
- Edge protector presence and position
- Strap-contact protection where required
- First-article surface review after actual transfer
- Final package review before release
- Changeover verification before coated production starts
This gives the project a defensible quality boundary without claiming universal damage-free results.
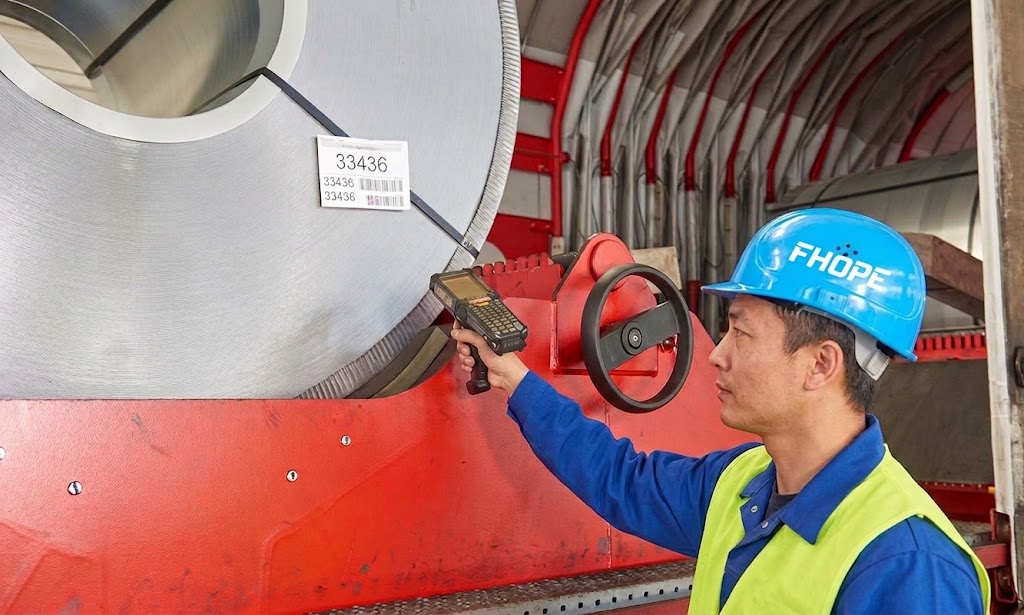
The image shows a labeling process on the packaging line. Final release for PPGI should confirm identity and label accuracy together with edge and surface checks, so the coil is not rejected later for a missing or mismatched record.
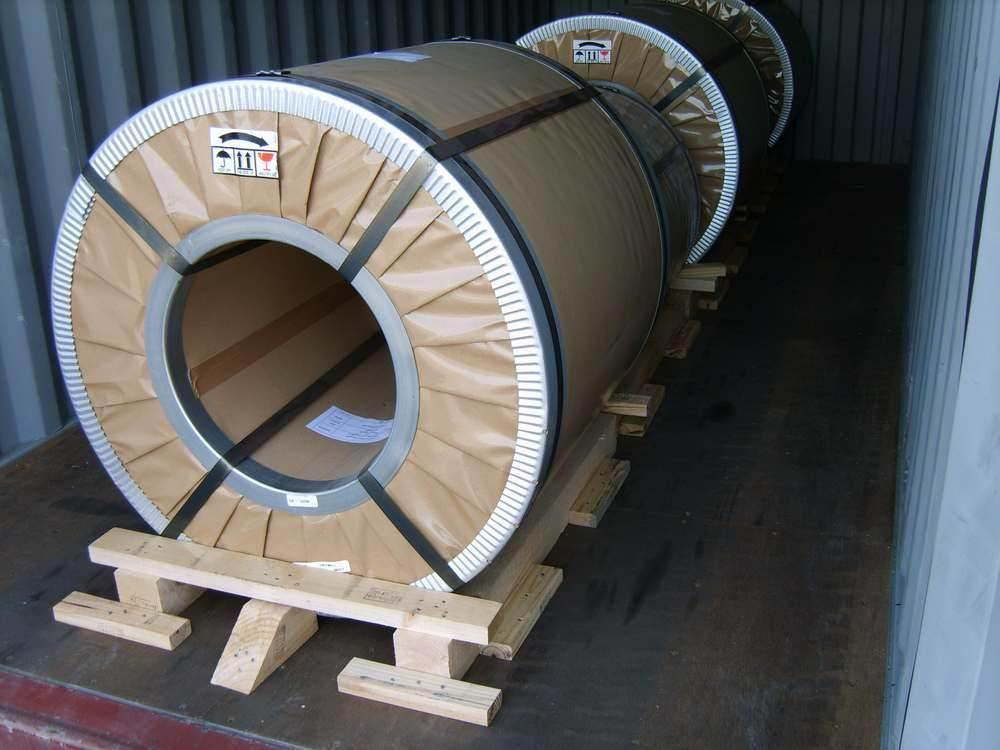
The image shows fully packaged steel coils prepared for shipment. The release record for PPGI should confirm the layer sequence, edge protection, strap-contact control, and changeover reset before the package leaves the line.
A Practical Next Step
Create a PPGI packaging recipe that shows the layer sequence, edge-protection rules, approved strap-contact devices, and coated-product changeover reset. Then validate it on a representative coated coil after the line has changed over from another product family on the automatic coil packing line, because that is where many hidden failures appear.
Visual Details
Click to enlarge
Click to enlarge

Click to enlarge
Click to enlarge
Watch How It Works
Discover how our automated packaging solutions optimize your production line efficiency. This video demonstrates the seamless operation designed for maximum protection.
Trusted by Steel Mills & Industry Leaders
Global manufacturers rely on FHOPE heavy duty packaging equipment


Ready to optimize your packaging line?
Get a custom quote with ROI analysis. Our engineers respond within 24 hours.
- Free layout design
- Global installation support
- 2-year warranty included
Your information is secure and will never be shared.
Related Machines
Steel Coil Packaging line
View Details →
Vertical coil packaging line
View Details →
Hose Coil Packaging line
View Details →
Copper Coil Packaging line
View Details →
Wire Coil Packaging line
View Details →
Panel Packaging line
View Details →
Pipe Bagging Machine
View Details →
Aluminum profile packing line
View Details →
FHOPE Automatic pipe tube bundling&strapping line
View Details →
Automatic pipe tube bundling & strapping line
View Details →
Automatic steel tube strapping machine
View Details →
FHOPE Automatic steel tube packing machine
View Details →
Automatic plastic Pipe strapping packing line
View Details →
Automatic PPR/PVC Pipe bagging line
View Details →
Platsic pipe bag packing machine
View Details →
Tyre Packing Machine FPT-200
View Details →
Tyre Packing Machine FPT-300
View Details →
Tyre Packing Machine FPT-400
View Details →
Cable Coil Packing Machine-FPCA100
View Details →